A year-long engineering project, a successful on-site installation, and a collaboration built on trust,
expertise, and a shared commitment to excellence.
Last August marked the completion of our latest on-site intervention at the Hassyan desalination plant in the United Arab Emirates, bringing another important milestone in a project that has been underway for over a year.
For Now Engineering Solutions, this project represents much more than a technical achievement. It is an opportunity to contribute our expertise to a major industrial facility, collaborate with internationally recognised companies, and continue growing through the challenges and knowledge that come with complex engineering projects.
We are particularly proud to have been entrusted with this assignment by ABB Spain and to have collaborated with SIDEM Veolia, a leading EPC contractor in the desalination sector. The confidence they have placed in Now Engineering Solutions is a source of great satisfaction and motivation, inspiring us to keep improving, expanding our expertise, and delivering increasingly effective solutions to our clients.
The project involved the engineering and implementation of a vibration monitoring system at the Hassyan desalination plant, one of the world’s major desalination facilities.
In an industrial environment where operational continuity is essential, protecting critical rotating equipment is a fundamental priority. Pumps and motors must operate reliably, often under demanding conditions, and even a relatively minor mechanical issue can develop into a more serious failure if it goes undetected.
The vibration monitoring system was designed to address these challenges by providing continuous condition monitoring, equipment protection, and advanced diagnostic capabilities.
By identifying abnormal vibration patterns and detecting potential mechanical issues at an early stage, the system supports predictive maintenance strategies, helping operators plan maintenance activities
before a fault escalates into an unexpected shutdown.
This approach can help reduce unplanned downtime, limit maintenance costs, protect valuable equipment, and minimise the risk of production interruptions — all key factors in a facility where reliability and efficiency are essential.
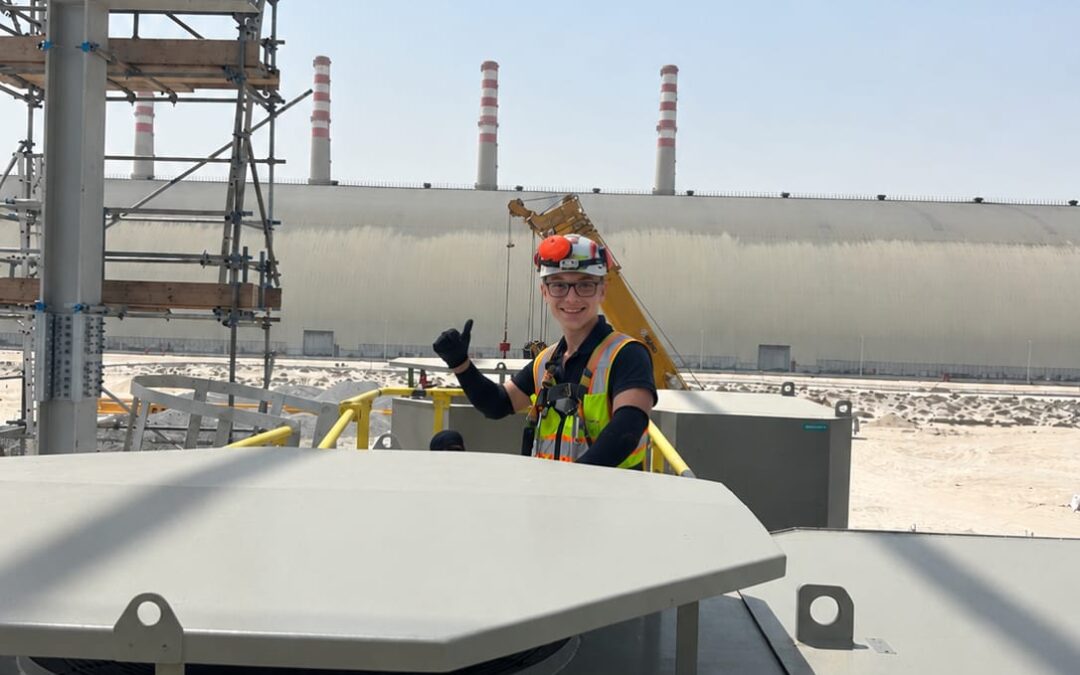
During our latest on-site intervention in August, our engineering team installed monitoring cabinets at different locations throughout the plant, together with more than 100 vibration sensors and their associated cabling.
These components form a key part of the monitoring infrastructure, enabling vibration data to be collected from critical machines and transmitted to the system for protection and diagnostic purposes.
Every component matters in an installation of this kind. Selecting the right sensors and cabling is particularly important in harsh industrial environments, where high temperatures, saline atmospheres,
and corrosive conditions can accelerate material degradation and compromise long-term reliability.
A monitoring system is only as dependable as the components on which it relies. For this reason, product quality, environmental suitability, and long-term performance are essential considerations from the very beginning of the engineering process.
For this project, we selected products manufactured by CTC, a brand we are proud to distribute.
The choice was driven by the importance of ensuring reliable measurement and robust performance in a demanding environment. In applications exposed to saline atmospheres, elevated temperatures, and corrosion, sensor and cable integrity is essential to maintaining the quality and continuity of monitoring over time.
Our latest site visit provided a particularly valuable opportunity to assess the installation after more than a year of service. We were delighted to find that all the installed sensors remained intact and in excellent condition, looking as good as new.
This real-world observation reinforced our confidence in CTC products and their suitability for demanding industrial applications. Beyond the initial specifications, long-term performance in the actual operating environment is one of the most meaningful indicators of product quality.
As proud CTC distributors, we are pleased to see this level of reliability confirmed in the field. We also greatly value our relationship with the CTC team, whose product excellence, transparent order management, collaborative approach, and outstanding availability have made them a trusted partner throughout our work.
The vibration sensors are interfaced with ABB MCM800 modules, which provide the system with important protection and diagnostic capabilities.
The modules incorporate relays that can be used to trigger protective actions when configured alarm or trip conditions are met. They also support specialised vibration diagnostics, helping maintenance teams
gain deeper insight into the condition of critical rotating machinery.
Another important feature is their direct integration with the plant’s Distributed Control System (DCS) through redundant PROFIBUS communication. This architecture enables the transfer of relevant
monitoring information without requiring conventional analogue outputs, such as 4–20 mA signals, for the supported integration functions.
The combination of reliable CTC sensors, ABB monitoring and protection modules, and a carefully engineered communication architecture provides a flexible and effective solution for machinery protection and condition monitoring.
By bringing together dependable field instrumentation, dedicated monitoring hardware, and integration with the plant control system, the solution supports a comprehensive approach to equipment reliability
and maintenance.
A Successful Project Built on Collaboration
At Now Engineering Solutions, we believe that successful engineering is not only about selecting the right technology. It is also about understanding the application, paying attention to the details, working
closely with all stakeholders, and building relationships based on trust and shared objectives.
This project has been a valuable opportunity to put that philosophy into practice.
We would like to express our sincere gratitude to ABB Spain for placing its trust in our services and giving us the opportunity to contribute to such an important project.
We are equally grateful to SIDEM Veolia for the collaboration and for the opportunity to work alongside their team.
We would also like to thank CTC for the quality and reliability of its products, as well as for its transparency, collaborative spirit, and continued support. Having partners who share our commitment to quality makes a real difference, particularly when working in demanding industrial environments.
Above all, we are grateful for the knowledge, technical experience, and personal growth this project has brought us. Every challenge has been an opportunity to learn, refine our approach, and strengthen our
capabilities. The trust established throughout this collaboration is something we genuinely value and hope to continue building on in future projects.
At Now Engineering Solutions, we are committed to helping our clients improve equipment reliability, optimise maintenance strategies, and find effective engineering solutions for their specific operational challenges.
Whether you are planning a new installation, upgrading an existing monitoring system, or looking for ways to improve the performance and reliability of critical machinery, our team would be pleased to discuss your requirements.
Get in touch with Now Engineering Solutions to explore ideas, discuss technical challenges, and identify solutions that can bring tangible value to your business and your projects.
We look forward to turning new challenges into successful engineering solutions — together.